Featured OEM/ODM Compacted & Dissolving Shampoo Formulations
Explore our export-ready range of solid shampoo tablets, ultra-thin dissolvable sheets, and custom packaging systems manufactured under audited ISO 22716 GMP standards.
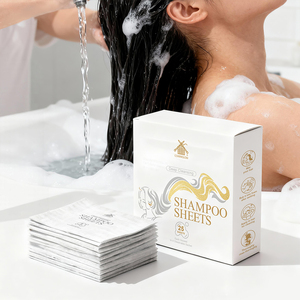
Portable Travel Pack 25 Tablets Travel Deep Clean Fast Dissolving Hair Shampoo Sheets
Anhydrous fast-dissolving shampoo sheets infused with zinc-based clarifying actives and botanical conditioners. Engineered for rapid water disintegration, itch relief, and compact travel packaging.
Contact Us
OEM ODM Menthol Solid Shampoo Tablets for Hotel & Fitness Amenities
Single-dose compressed shampoo tablets featuring natural cooling menthol. Formulated for high-lather performance in boutique hotel guest rooms, luxury resorts, and high-end executive fitness centers.
Contact Us
Private Label Menthol Solid Shampoo Tablets for Luxury Travel Kits
Compact solid shampoo formulation designed for airline amenity kits and hotel groups. Zero-water recipe eliminates spill risks during transit while providing a scalp-invigorating menthol wash.
Contact Us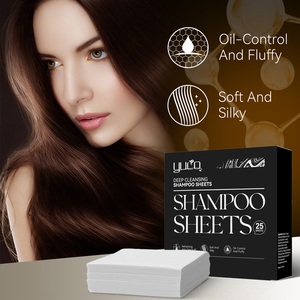
Natural Nourishing & Moisturizing Dissolving Hair Shampoo Sheets
Enriched with natural lipids, amino acids, and scalp conditioners. Restores moisture balance to dry hair while preventing dandruff. Ideal for eco-conscious retail consumer brands.
Contact Us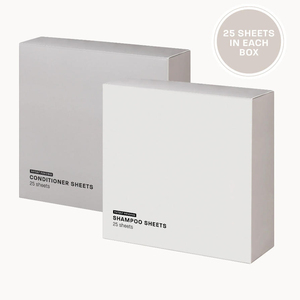
Portable Eco-Friendly Dissolvable Shampoo Paper Tablets
Ultra-lightweight paper shampoo technology designed for outdoor, backpacking, and eco-travel markets. Instant water-activation generates rich foam with zero single-use plastic waste.
Contact Us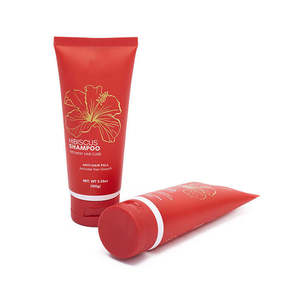
Custom PE Soft Squeeze Tubes (50ml) for Travel & Hotel Amenities
Flexible 50ml PE packaging tubes suitable for liquid or tablet formulations. Features custom color matching, offset silk-screen printing, and secure flip-top seal caps for hospitality programs.
Contact Us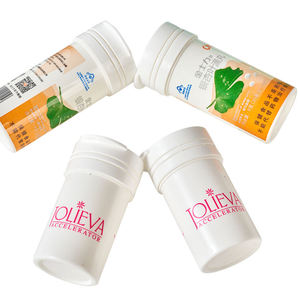
High-Barrier Effervescent Tablet Packaging Tubes with Moisture Lock
Rigid protective plastic tubes equipped with integrated desiccant stoppers. Prevents humidity degradation and maintains stability for compressed shampoo and cleaning tablets across a 24+ month shelf life.
Contact Us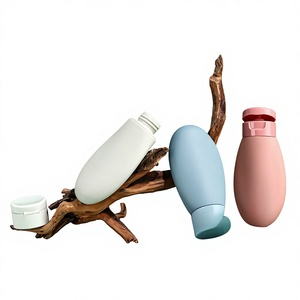
Matte-Finish PE Soft Squeeze Tubes with Custom Screen Printing
Aesthetic, soft-touch matte PE tubes designed for luxury hotel amenities and retail skincare collections. Compatible with waterless paste, concentrated gels, and mini tablet travel kits.
Contact UsThe Engineering of Anhydrous Haircare: Formulation, Compression, & Global Procurement Optimization
The global personal care and hotel amenity landscape is experiencing an unprecedented structural pivot toward waterless, solid, and compacted formulations. Historically, liquid shampoos containing 80% to 90% water dominated both retail shelves and commercial hospitality supply chains. However, tightening global plastic regulations, escalating oceanic freight tariffs, and carbon-reduction corporate mandates have converted compacted shampoo tablets from a niche natural cosmetics alternative into a mainstream B2B manufacturing imperative.
1. Formulation Chemistry: Anhydrous Surfactant Binding & Effervescent Disintegration
Developing commercially viable shampoo tablets requires balancing mechanical hardness (to resist crumbling during transit) with ultra-rapid water disaggregation upon user application. Unlike conventional soap bars produced through saponification, compressed shampoo tablets are formulated using dry syndet (synthetic detergent) chemistry.
Our R&D formulation matrix relies on high-purity primary surfactants such as Sodium Cocoyl Isethionate (SCI) or Sodium Lauryl Sulfoacetate (SLSA), blended with micro-crystalline cellulose binders and plant-derived conditioners (such as hydrolyzed wheat protein, guar hydroxypropyltrimonium chloride, and natural betaine). To achieve instant lathering under shower stream conditions, micro-effervescent couples—combining cosmetic-grade citric acid and sodium bicarbonate—are precisely calibrated to drive rapid tablet disintegration upon hydration.
Anhydrous Compression
High-tonnage rotary tablet pressing compacts active powders into dense, highly stable tablets without degrading sensitive botantical extract profiles or natural menthol actives.
Preservative Minimization
Because free water activity ($a_w$) is reduced to near zero (<0.2), microbial proliferation is inherently suppressed, allowing for gentler, preservative-free or natural preservative matrices.
Climate-Controlled Packing
Anhydrous tablets are compressed under low-humidity cleanroom environments and sealed in high-barrier desiccant tubes or aluminium foils to prevent premature atmospheric hydration.
2. Comparative Performance Matrix: Liquid vs. Solid vs. Compacted Tablet Shampoo
For global brand managers, procurement directors, and hotel chain buyers, understanding the structural and technical differences across haircare delivery formats is essential for portfolio optimization:
| Performance Specification | Conventional Liquid Shampoo | Extruded Solid Shampoo Bars | Compacted OEM Shampoo Tablets |
|---|---|---|---|
| Water Content ($H_2O$) | 80% – 90% | 5% – 15% | < 1% (Anhydrous) |
| Single-Dose Precision | Variable (User Poured) | Multi-Use Bar (Hygiene Concerns in Hotels) | 100% Exact Single-Dose Unit |
| Microbial Contamination Risk | Moderate to High (Requires Strong Preservatives) | Low to Moderate (Post-Use Moisture Retention) | Zero In-Package Microbial Risk |
| Freight Payload Efficiency | Baseline (Shipping Water Weight) | 3x Efficiency Improvement | 8x to 10x Max Freight Density |
| Plastic Packaging Reliance | High (PET/HDPE Bottles) | Low (Paper Wrap / Paper Box) | Zero Plastic (Desiccant Tubes / Foil Sachets) |
| Regulatory Compliance (EU/US) | Liquid Volume Limits (TSA 100ml) | Unrestricted Travel Solid | Unrestricted Solid / Travel Approved |
Future Procurement & Development Trends in Solid Haircare (2025–2030)
1. Regulatory Legislation Driving Hospitality & Retail Procurement
Governments worldwide are enacting aggressive environmental legislation targeting single-use cosmetic packaging. Measures such as California Assembly Bill 1162 and the European Union’s Packaging and Packaging Waste Regulation (PPWR) explicitly restrict hotel chains from distributing miniature single-use plastic bottles (under 50ml). Concurrently, global luxury hotel chains (including Wyndham, Radisson, Caesars Palace, and Extended Stay America) are revising global amenity standards. Compacted shampoo tablets provided in eco-friendly tubes or paper sachets present the ultimate compliant solution for hospitality guest rooms.
2. Consumer Demand for Precision Dosing & Active Stabilization
Modern retail consumers are increasingly educated regarding active ingredient degradation in aqueous solutions. Bioactive compounds—such as L-Ascorbic Acid (Vitamin C), Niacinamide, Salicylic Acid, natural Menthol, and sensitive botanical peptides—oxidize rapidly when submerged in liquid water over extended retail shelf lives. Compacted anhydrous tablet technology immobilizes these delicate active ingredients inside a dry matrix, ensuring maximum potency upon water activation during washing.
3. Strategic Sourcing Migration to Southeast Asian Manufacturing Hubs
As Western buyers seek to diversify cosmetic contract manufacturing supply chains away from single-source markets, Malaysia has established itself as the leading high-tier OEM/ODM personal care manufacturing center in Asia. Positioned strategically within ASEAN, Malaysian contract manufacturing facilities combine advanced European chemical engineering with RSPO-certified sustainable palm oil sourcing, ISO 22716 GMP cleanrooms, JAKIM Halal compliance, and competitive export tariff structures to North America and Europe.
Enterprise Advantages: HE Manufacturing (M) Sdn Bhd
Italian Formulation Expertise Combined with Malaysia's World-Class Manufacturing Infrastructure.
Founded in 2012 in Rawang, Selangor, Malaysia, HE Manufacturing (M) Sdn Bhd operates as an internationally audited OEM, ODM, and contract manufacturer specializing in personal care, hair care, bar soap, wet & dry hotel amenities, and waterless cleaning tablet technology. Operating under European leadership led by Chief Executive Officer Elisa Polidoro, our facility blends Italian aesthetic design and formulation rigor with Malaysian manufacturing efficiency.
Comprehensive Audited Certifications
Fully audited production environment operating under ISO 9001 quality systems, ISO 22716 Cosmetics GMP, JAKIM Halal certification, RSPO (Sustainable Palm Oil) membership, and registered as a US MoCRA Compliant Facility.
In-House R&D & Stability Testing
Our dedicated formulation laboratory manages 5-condition accelerated stability testing, preservative efficacy testing (PET), micro-challenge testing, and custom scent development—retaining 100% client formulation IP protection.
Turnkey Export Logistics
Supplying over 50 major hotel brands and retail distributors across 20+ countries (including the US, EU, UK, Canada, Australia, Middle East, and Asia-Pacific). We coordinate compliance labeling, MSDS, COA, and export documentation end-to-end.
Frequently Asked Questions (B2B Sourcing FAQ)
Essential technical and operational answers for brand owners, buyers, and sourcing managers.
Q1: What is the Minimum Order Quantity (MOQ) for private label shampoo tablet manufacturing?
Our MOQs are structured flexibly to accommodate scaling brands, regional hotel chains, and major retail importers. Depending on tablet diameter, active formulation complexity, and primary packaging selection (desiccant tubes vs. individual foil sachets), standard production runs start from low pilot batches up to full container programs.
Q2: How fast do compacted shampoo tablets dissolve in shower conditions?
Our R&D team formulates shampoo tablets for rapid disaggregation. When crushed lightly in wet hands or exposed directly to shower water, micro-effervescent couples break down the compressed tablet within 3 to 5 seconds, forming a rich, creamy lather equivalent to 10ml to 15ml of high-end liquid shampoo.
Q3: How are anhydrous tablets protected against environmental humidity during transport and storage?
Atmospheric moisture is prevented through specialized high-barrier packaging options. We offer medical-grade rigid plastic tubes with desiccant-integrated caps, sealed aluminum tubes, and multi-layer recyclable barrier foils tested to maintain product integrity across extreme temperature and humidity cycles ($40^\circ\text{C} / 75\%\text{ RH}$).
Q4: Can HE Manufacturing custom-formulate scents, colors, and active ingredient complexes?
Yes. We provide full ODM (Original Design Manufacturing) services. Our in-house chemical engineers can customize fragrance profiles (essential oil blends or synthetic allergen-free perfumes), natural color pigments, and functional active ingredient complexes (anti-dandruff, scalp soothing, color-safe, or deep hydration).
Q5: What compliance documentation is provided for international custom clearance?
Every production batch is accompanied by a full Certificate of Analysis (COA), Safety Data Sheets (SDS / MSDS), Technical Data Sheets (TDS), INCI Ingredient Lists, and Stability Testing Reports. For US export, facilities are MoCRA registered; for EU export, documentation supports your designated Responsible Person (RP).
Q6: What is the difference between OEM and ODM manufacturing partnerships with your factory?
OEM (Original Equipment Manufacturing) applies when you supply your proprietary formula or detailed technical specifications for production. ODM (Original Design Manufacturing) applies when our R&D team develops the formulation, fragrance, tablet shape, and packaging concept based on your initial brand brief.
Launch Your Waterless Haircare or Hospitality Range Today
Partner with an ISO 22716 GMP, Halal, and US MoCRA registered manufacturer in Malaysia. Connect directly with our engineering and procurement team for custom formulation samples, packaging solutions, and tiered B2B quotations.
Contact Us