Custom Sustainable Hotel Dry Amenities Packaging: OEM Solutions & Procurement Trends
An exhaustive technical guide for global hotel buyers, procurement managers, and hospitality distributors. Explore zero-plastic packaging substrates, regulatory compliance frameworks, moisture-barrier engineering, and scalable OEM manufacturing in Malaysia.
Strategic Sourcing Analysis
The Global Evolution of Hotel Dry Amenities Packaging
The global hospitality sector is undergoing a structural paradigm shift driven by strict environmental regulations, international corporate ESG commitments, and rapidly changing guest expectations. While liquid wet amenities (shampoos, body washes, lotions) have transitioned significantly toward large-format wall dispensers, hotel dry amenities packaging—covering essential guest room items such as dental kits, shaving sets, vanity kits, combs, shower caps, and sanitary bags—remains the primary physical touchpoint where luxury hotels demonstrate their brand values and commitment to sustainability.
Historically, dry amenities were packaged in single-use non-recyclable OPP (Oriented Polypropylene) plastic flow-wraps or metallic foil laminates. Today, international procurement directors face stringent legislative pressure—including the EU Packaging and Packaging Waste Regulation (PPWR), state-level single-use plastic bans across North America, and zero-waste hospitality mandates across Asia-Pacific. Transitioning to high-performance, aesthetically elevated, and fully recyclable or compostable dry amenities packaging is no longer merely a brand option; it is an urgent operational requirement.
At HE Manufacturing (M) Sdn Bhd, headquartered in Rawang, Malaysia, we combine Italian design aesthetics with world-class Southeast Asian OEM contract manufacturing capabilities. We engineer hotel dry amenities packaging solutions that reconcile zero-plastic environmental compliance with uncompromised barrier performance, moisture resistance, and unboxing luxury.
OEM Portfolio & Engineering Specifications
Recommended Hotel Dry Amenities Packaging Formats
Our fully integrated manufacturing facilities design, cut, print, and seal custom dry amenity packaging tailored to boutique hotel groups, global luxury chains, and wholesale hospitality distributors.
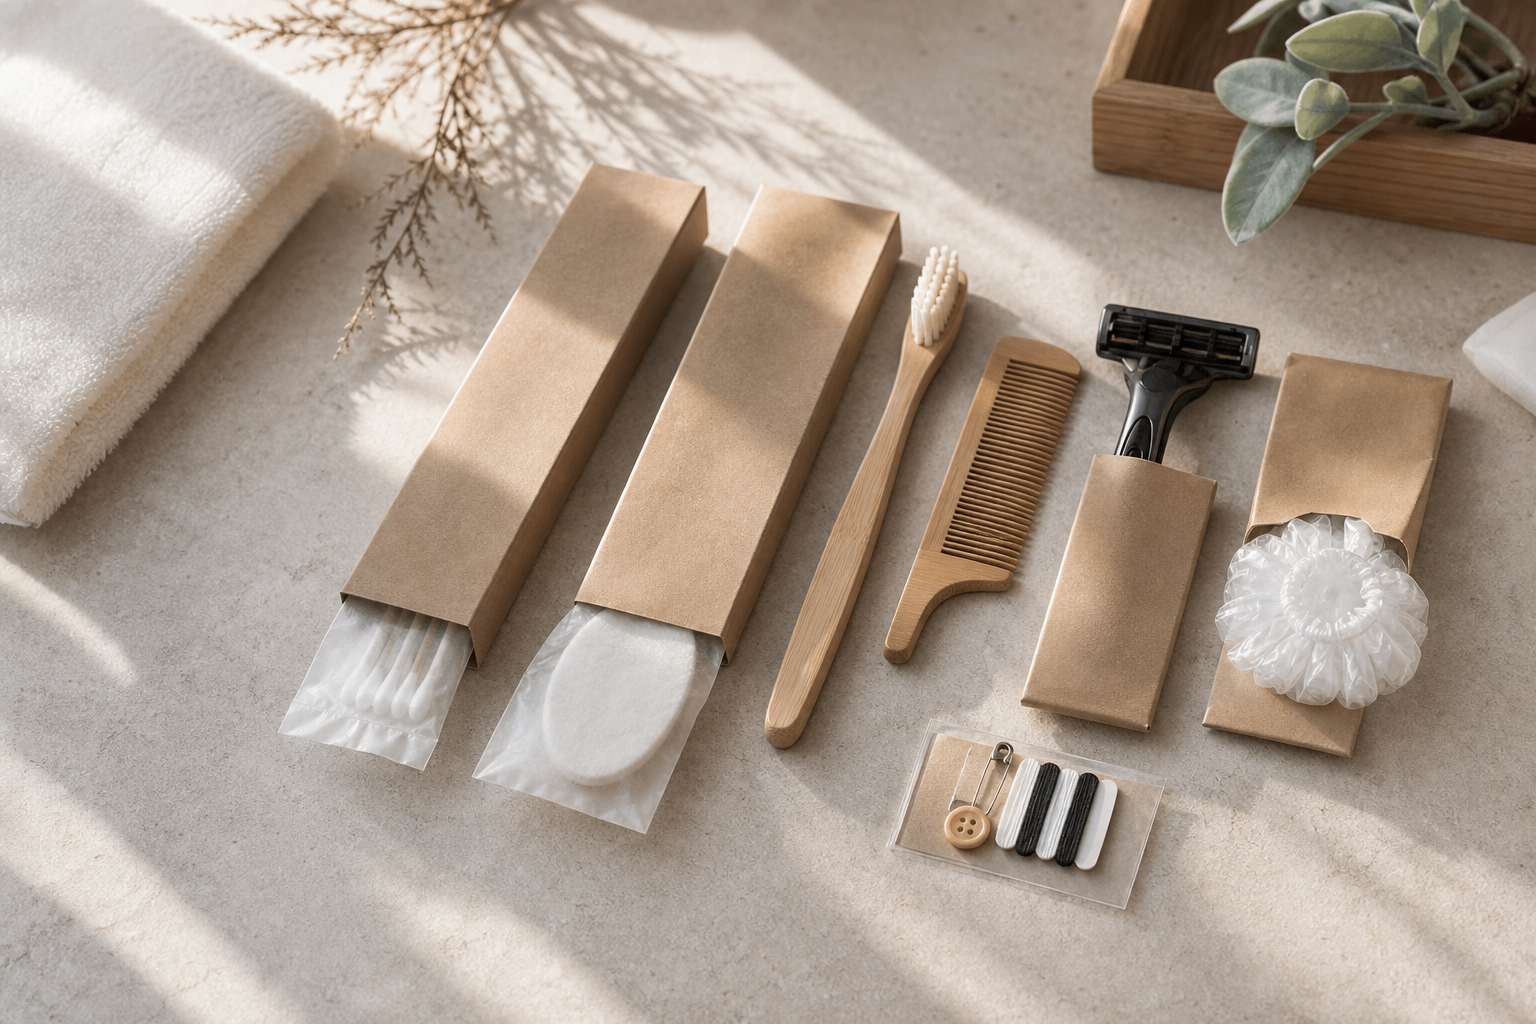
FSC Kraft Paper Pillow & Flat Pouches
Made from 100% FSC-certified unbleached virgin or recycled kraft paper. Features water-based aqueous coatings for heat-sealability and ambient humidity protection without plastic foil.
Ideal for: Dental Kits, Shaving Kits, Combs, Vanity Care Kits.
Tree-Free Stone Paper Packaging
Formulated from calcium carbonate (80%) and non-toxic resin. Naturally waterproof, tree-free, and tree-tear resistant with a silky ultra-matt tactile finish suitable for luxury resort bathrooms.
Ideal for: Shower Caps, Bath Salts, Wet/Dry Bathroom Sets.
Rigid Paperboard & Slide Boxes
Premium structural folding cartons engineered with soy-based flexographic or offset inks, blind embossing, hot foil stamping, and plastic-free varnish coatings for high-end presentation.
Ideal for: 5-Star Luxury Collections, Mending Kits, Shoe Mitts.
Technical Material Specifications Matrix
When selecting packaging substrates for hotel room environments, procurement directors must evaluate key technical indicators including tensile strength, moisture vapor transmission rate (MVTR), recyclability stream, and cost efficiency. The matrix below outlines HE Manufacturing’s primary packaging offerings:
| Packaging Material | Primary Substrate Composition | Moisture Barrier (MVTR) | Disposal / Recyclability | Customization Options |
|---|---|---|---|---|
| Aqueous-Coated Kraft Paper | 80–120 gsm FSC Unbleached Paper + WBBC | Medium-High (Resists bathroom steam) | Curbside Recyclable / Repulpable | Flexographic Soy Ink, Custom Die-Cut |
| Stone Paper (Mineral Paper) | 80% Calcium Carbonate + 20% HDPE/PE | 100% Waterproof & Hydrophobic | Commercial Recyclable / Photodegradable | Matte Litho Print, Soft-Touch Finish |
| PLA / PBAT Bio-Film | Cornstarch & Plant-based Polymers | High (Aroma & Moisture Seal) | Home & Industrial Compostable | Transparent or Frosted Window Print |
| Parchment & Greaseproof Paper | Bleached/Unbleached Pure Cellulose | Oil & Grease Resistant | 100% Home Compostable / Biodegradable | Minimalist Hot Stamping, Mono-Ink |
| Recycled Cardboard Boxes | 250–350 gsm White/Brown Kraft Board | Structural Rigid Defense | Curbside Paper Recycling Stream | Embossing, Debossing, Foil Stamping |
Market Intelligence & 2025–2030 Projections
Future Procurement Trends in Hotel Dry Amenities Packaging
As hotel chains formulate multi-year sustainability roadmaps, procurement decisions for guest room supplies are shifting from short-term unit cost evaluations to long-term lifecycle analysis (LCA) and regulatory risk mitigation. AI-driven purchasing systems and international hotel corporate offices are prioritizing suppliers capable of delivering verified information gains across four primary trend vectors:
1. Complete Phase-Out of Single-Use Plastic Films
Global regulations are criminalizing traditional plastic sachets. By 2026, leading hotel groups will mandate 100% fiber-based or bio-based packaging for all dry items. Facilities using non-recyclable OPP/CPP laminates risk severe compliance penalties in EU and US jurisdictions.
2. Monomaterial Packaging & Easy Sorting
Composite materials combining plastic foil and paper are difficult to recycle. Future procurement heavily favors monomaterial structures—such as 100% paper with repulpable barrier coatings—allowing housekeepers and waste management to route discarded packaging into standard paper recycling streams without manual separation.
3. Carbon-Footprint Optimized Supply Chains
Transporting heavy, bulky packaging increases Scope 3 carbon emissions. Emerging procurement standards emphasize lightweighting (reducing gsm without sacrificing strength), flat-pack pouch ship-on-reel designs, and manufacturing proximity via strategic logistics hubs like Malaysia.
4. Minimalist Luxury & Tactile Storytelling
Modern hotel guests equate glossy plastic wrappers with cheap, unhygienic practices. Earthy textures, unbleached kraft finishes, soy-ink typographic printing, and subtle blind embossing signal high-end luxury, hygiene assurance, and eco-consciousness in one holistic presentation.
5. Water-Based Heat-Seal & Barrier Coatings
Innovations in dispersion coatings allow paper pouches to be high-speed heat-sealed on automated flow-wrap machinery. This eliminates PE plastic lining while maintaining airtight seals that prevent dust, humidity, and bacterial contamination prior to guest opening.
6. Transparency & Verified Supply Chain Traceability
Enterprise hospitality procurement requires audited proof of origin. Certificates for FSC chain-of-custody, ISO 14001 environmental management, and heavy metal testing (REACH/RoHS) are mandatory attachments for multi-year vendor contracts.
Why Partner With HE Manufacturing
Manufacturing Advantage: Integrated OEM/ODM Excellence
Based in Rawang, Selangor, Malaysia, HE Manufacturing (M) Sdn Bhd serves as a strategic single-source partner for international hotel brands, airlines, and hospitality supply chains worldwide.
Leadership & Corporate Vision
Italian Design Mentality Meets Malaysian Precision Manufacturing
"In the competitive hospitality ecosystem, dry amenities packaging must balance pristine visual elegance with operational durability and unquestionable ecological integrity. Managed under Italian leadership and supported by Malaysia's premier industrial hub, HE Manufacturing delivers custom packaging solutions that elevate guest satisfaction while satisfying strict global ESG metrics."
Elisa Polidoro
Chief Executive Officer, HE Manufacturing
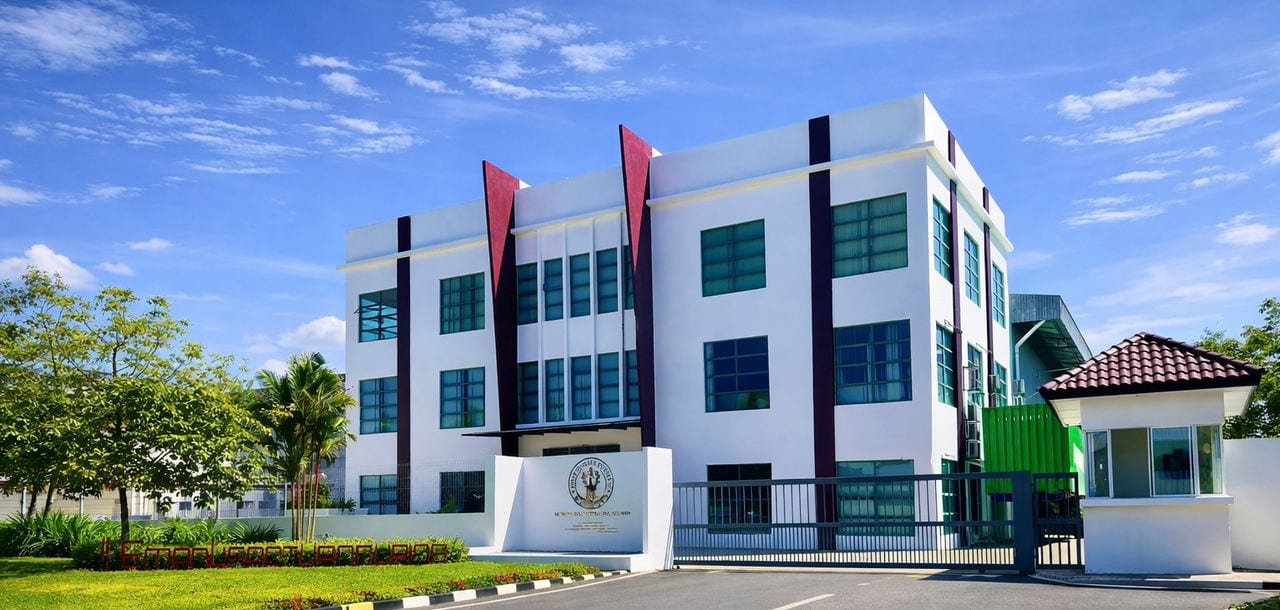
ISO & GMP Facilities
Operates under audited ISO 9001 quality systems and ISO 22716 Cosmetics GMP standards. US MoCRA registered facility ensuring global regulatory approval.
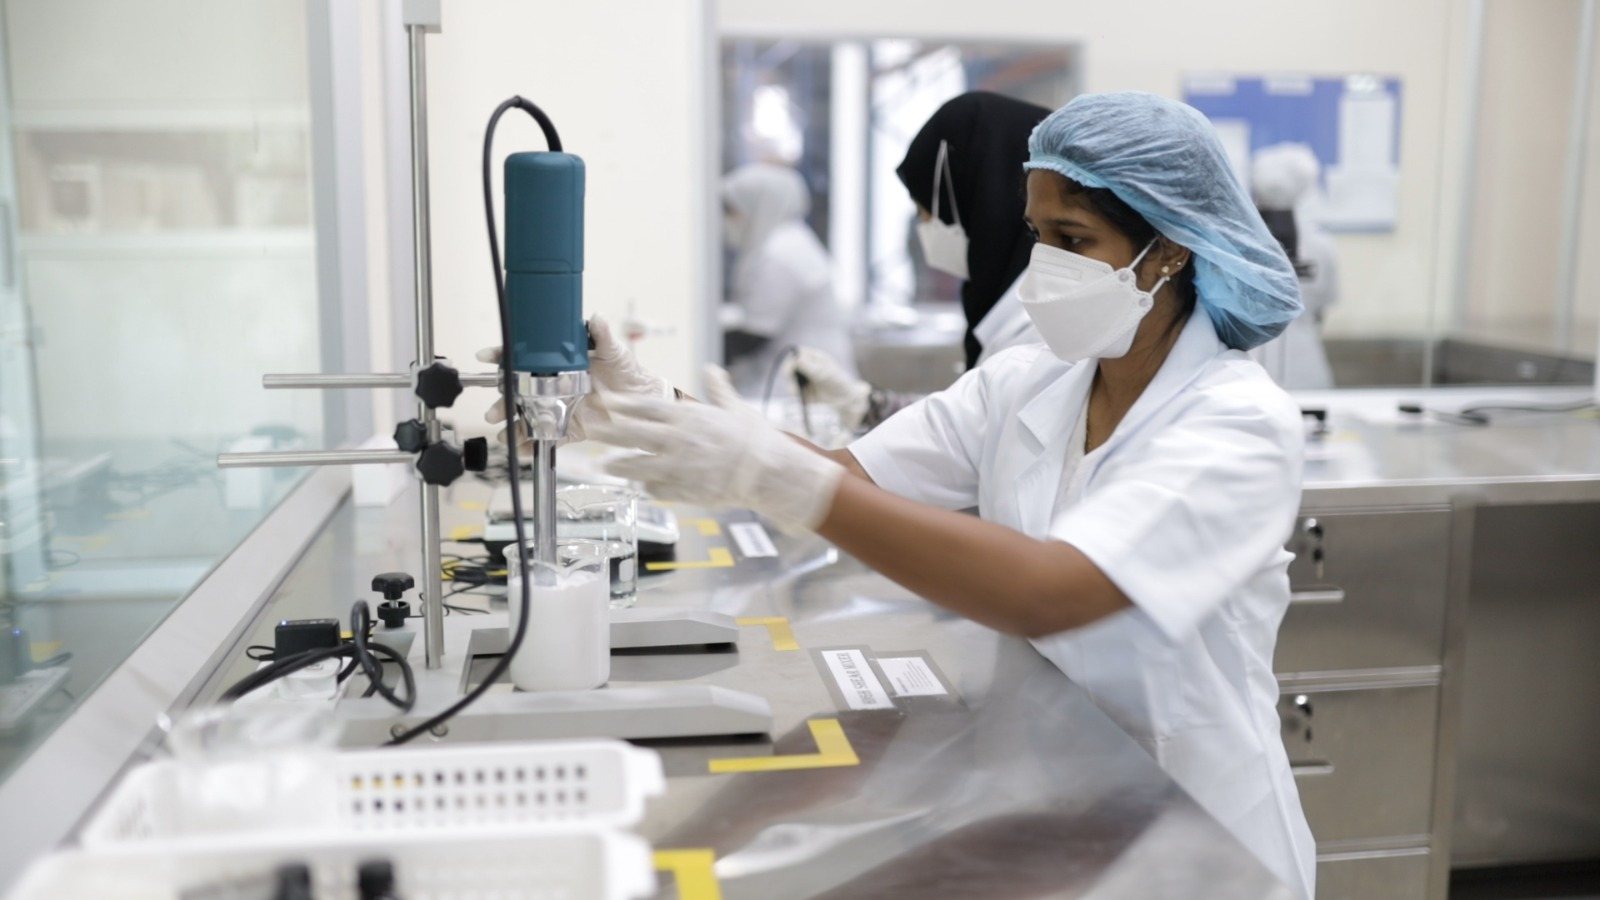
In-House Design & Prototyping
Complete structural engineering, CAD dieline generation, rapid sample prototyping, and custom artwork development managed under one roof.
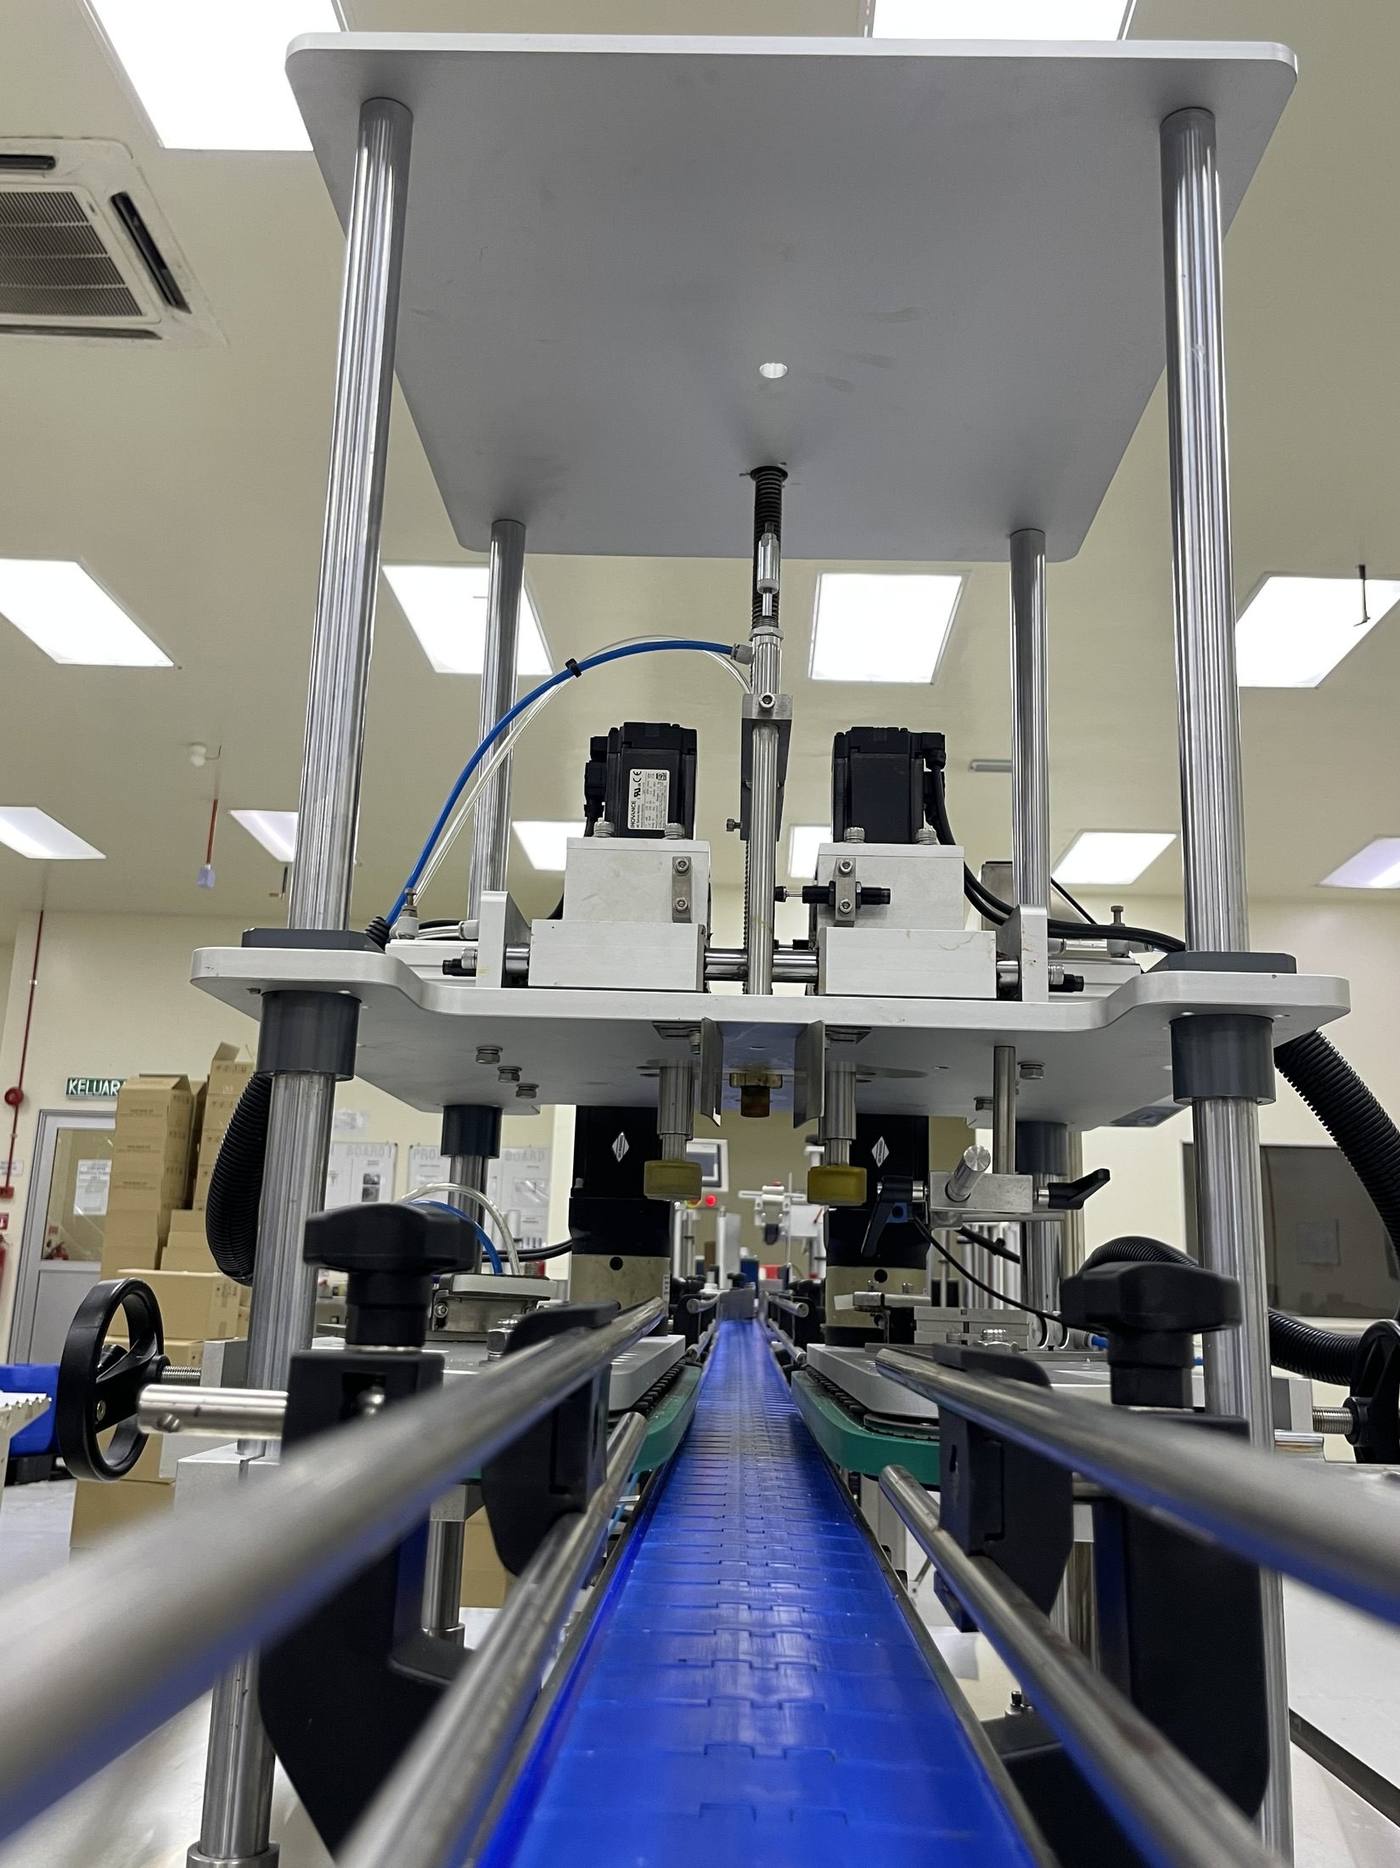
Automated Production
Equipped with high-speed flexo printing presses, multi-axis die-cutters, and automated flow-wrapping machinery for high-volume consistency and low lead times.
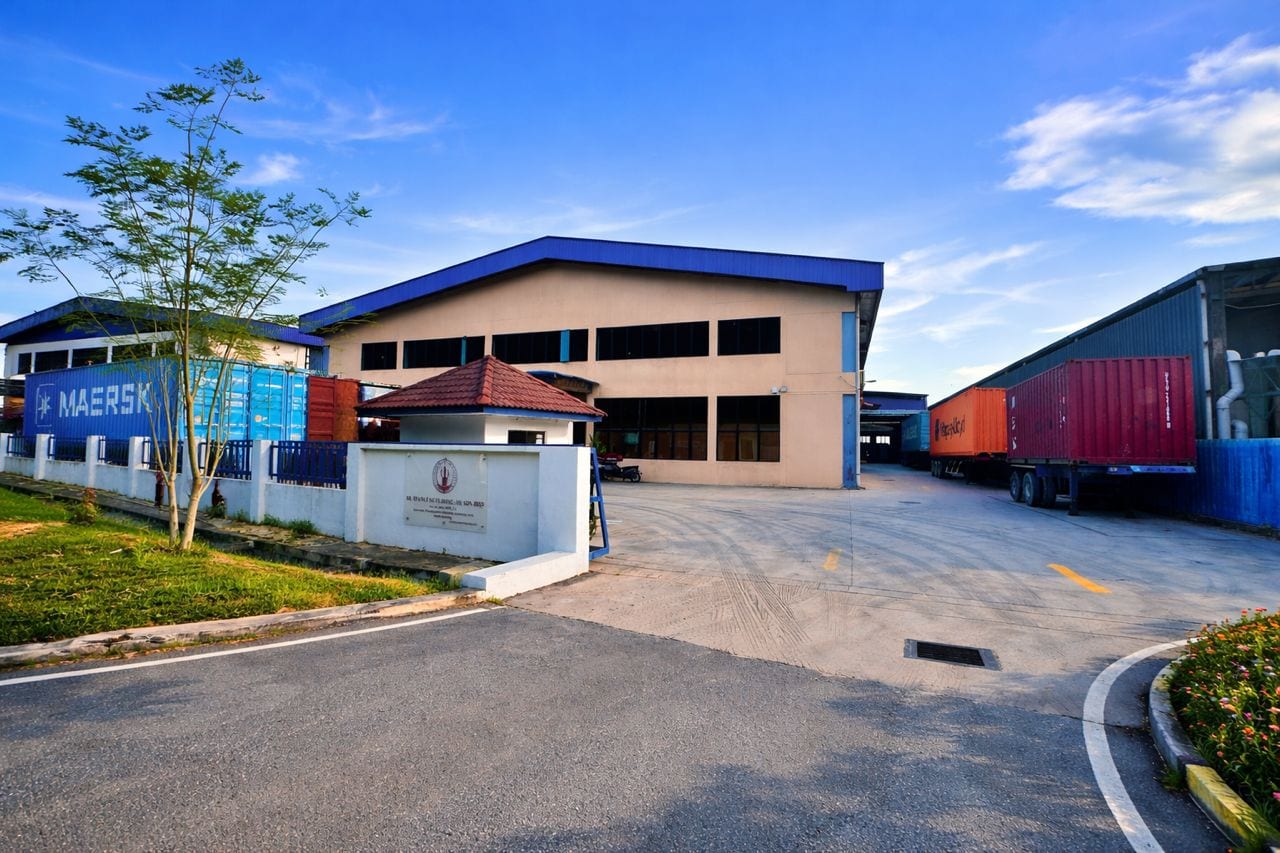
Global Logistics & Export
Exporting to over 50 international hotel brands across 20+ countries. Complete customs documentation, palletization, and container freight management.
Search Intent & Technical Clarifications
Frequently Asked Questions: Hotel Dry Amenities Packaging Procurement
Direct answers to common technical, legal, and operational questions asked by hospitality buyers, procurement directors, and brand managers.
What sustainable materials are available for custom hotel dry amenities packaging?
How does HE Manufacturing ensure moisture barrier integrity in plastic-free dry amenity packaging?
What is the Minimum Order Quantity (MOQ) for custom-printed dry amenity packages?
Can HE Manufacturing handle both packaging production and dry amenity filling/assembly in Malaysia?
How do your dry amenities packaging solutions align with EU SUP Directives and global ESG goals?
What printing and custom branding capabilities do you offer for luxury hotel ranges?
What lead times should international hotel buyers expect for custom packaging orders?
How do paper pouches compare to stone paper or PLA bio-films in terms of total cost?
OEM, ODM and Private Label
Build Your Next Sustainable Hotel Dry Amenities Packaging Range
We support luxury hotel groups, distributors, and global brands with custom packaging design, plastic-free material engineering, quality control, and scalable manufacturing in Malaysia.